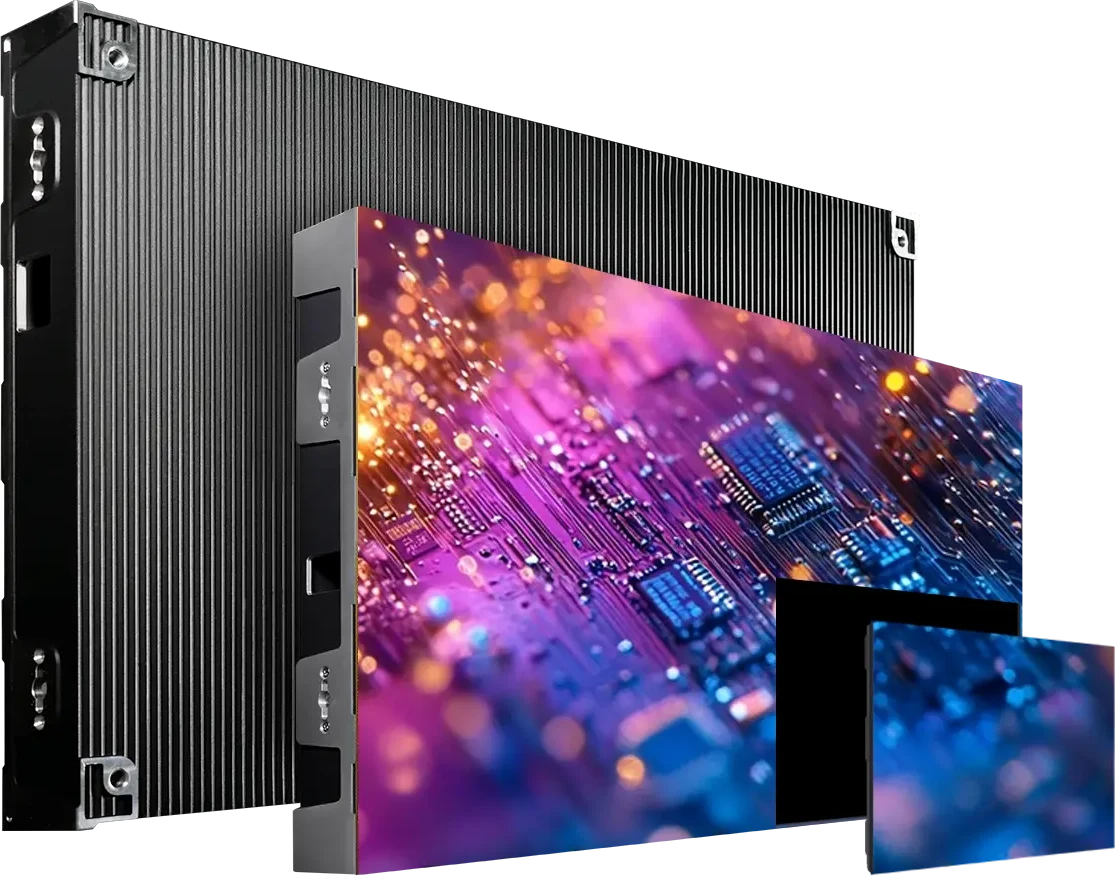
dvLED panels, grouped by the technology on their surface
How the LEDs are mounted decides almost everything you care about: contrast, durability, how fine the pitch can go, how the dvLED wall is serviced and what it costs. So the catalogue is laid out that way rather than by product name.
Every panel is developed, assembled and calibrated in Europe, specified component by component to our own module logic, and driven by our own ERMAC control system, so the two were designed for each other rather than made to tolerate each other.
COB, MIP, SMD and IMD: four ways to mount an LED
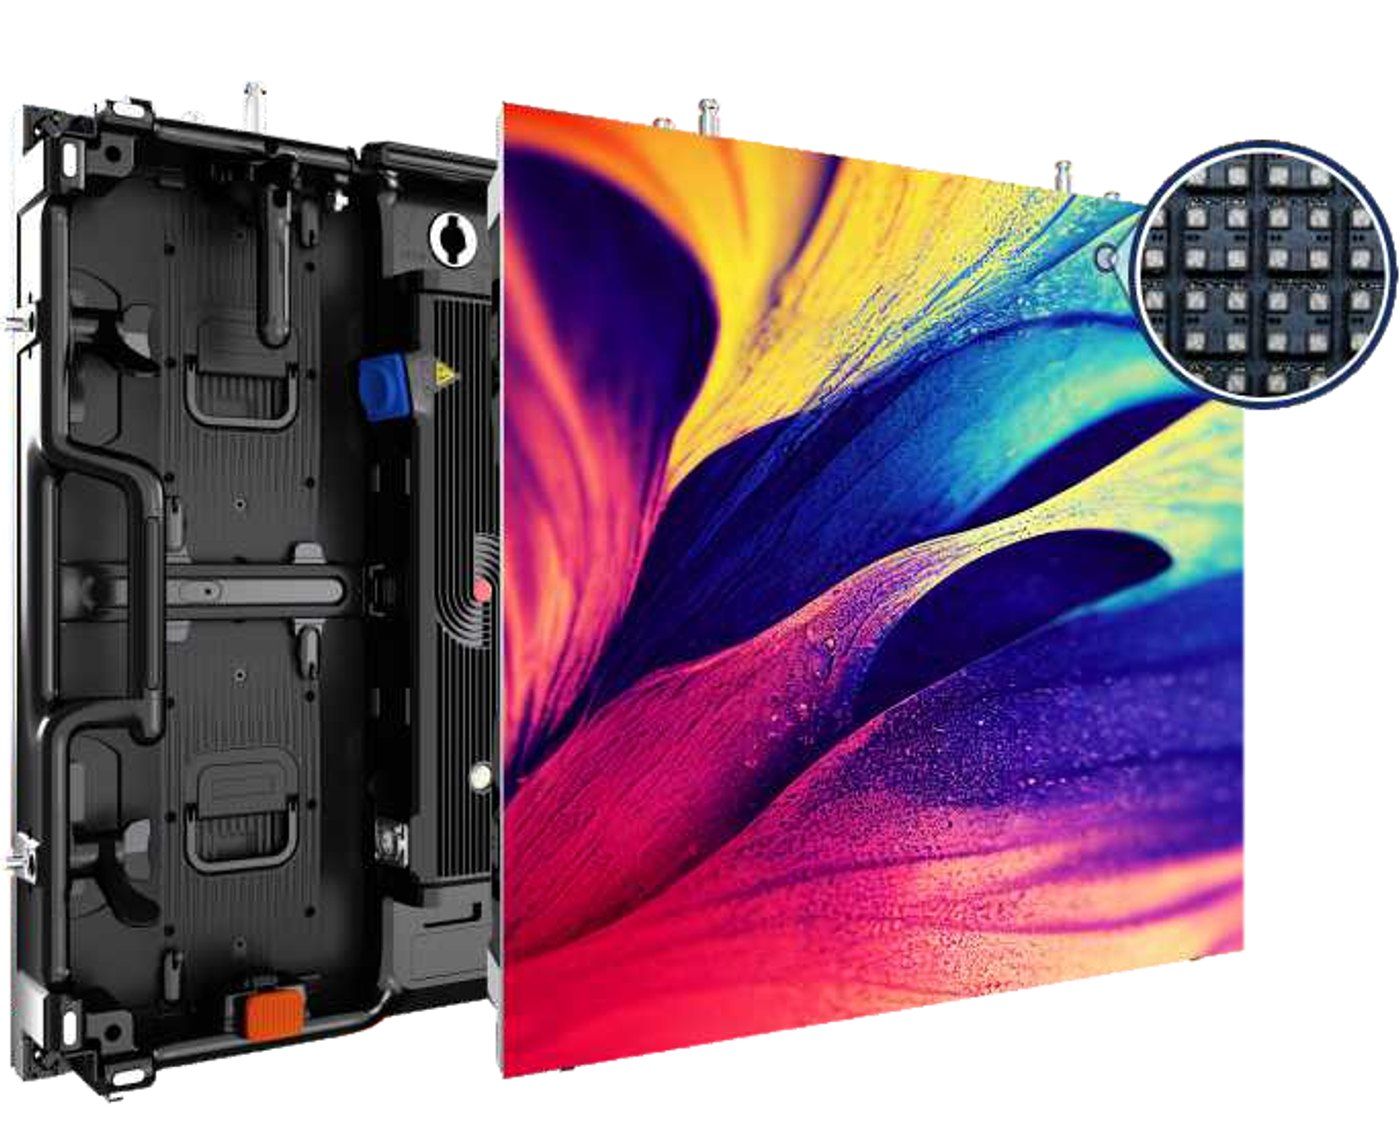
Same dvLED wall, four different surfaces. What changes is how the LEDs are mounted, and that decides contrast, durability, how fine the pitch can go and what it costs.
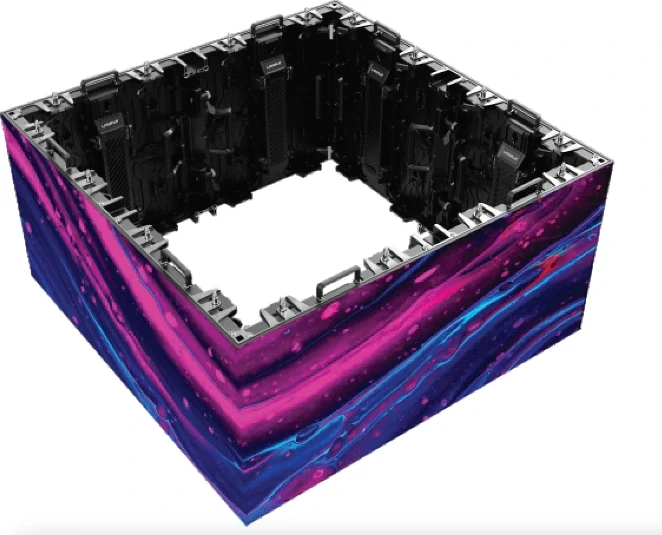
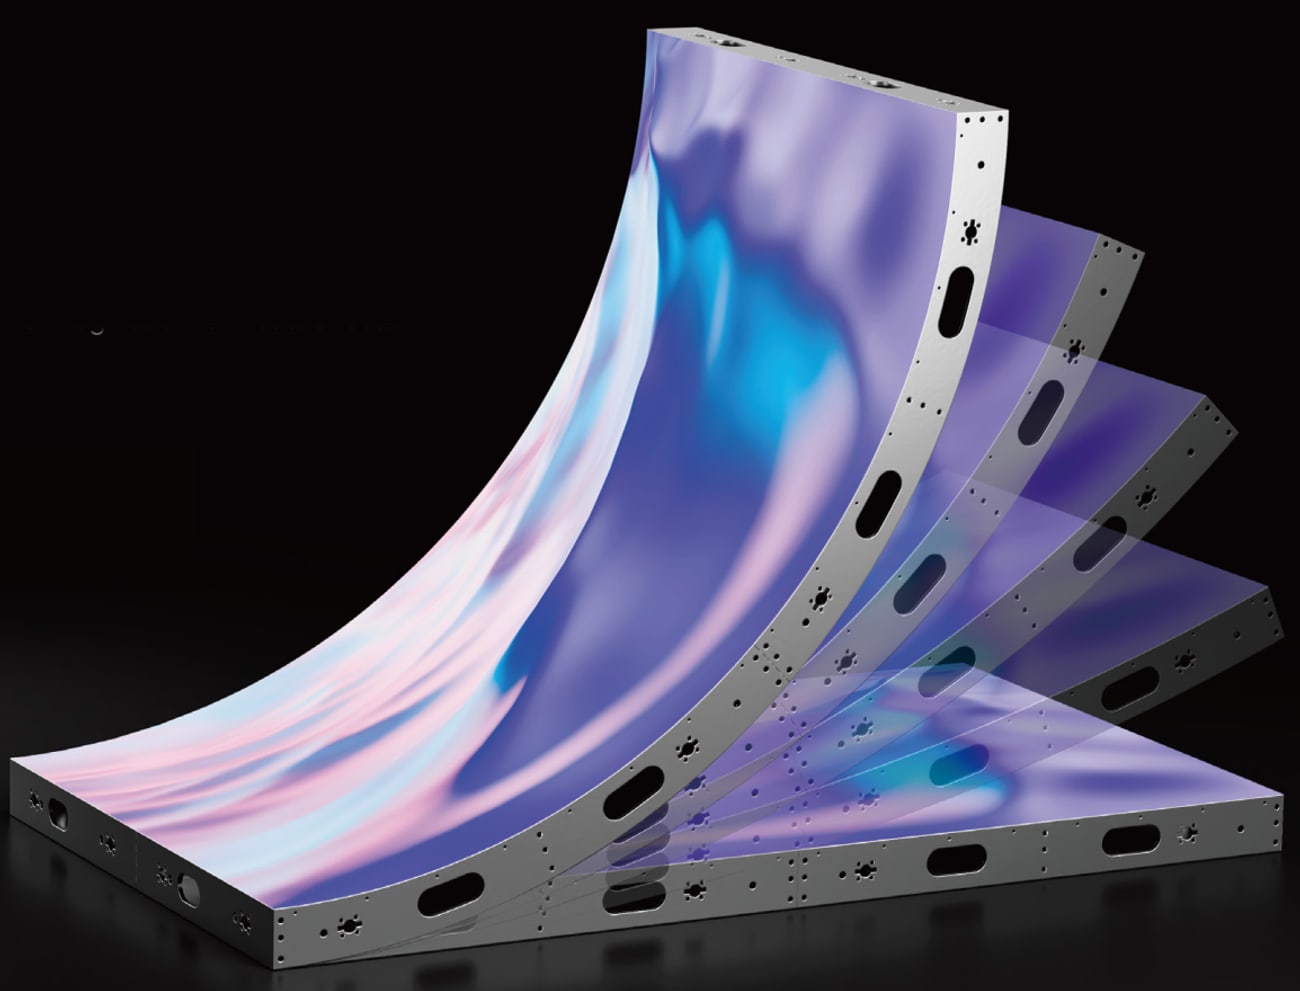
Any of those surfaces, in any of these shapes
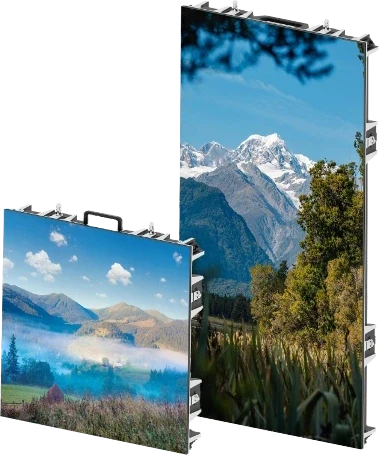
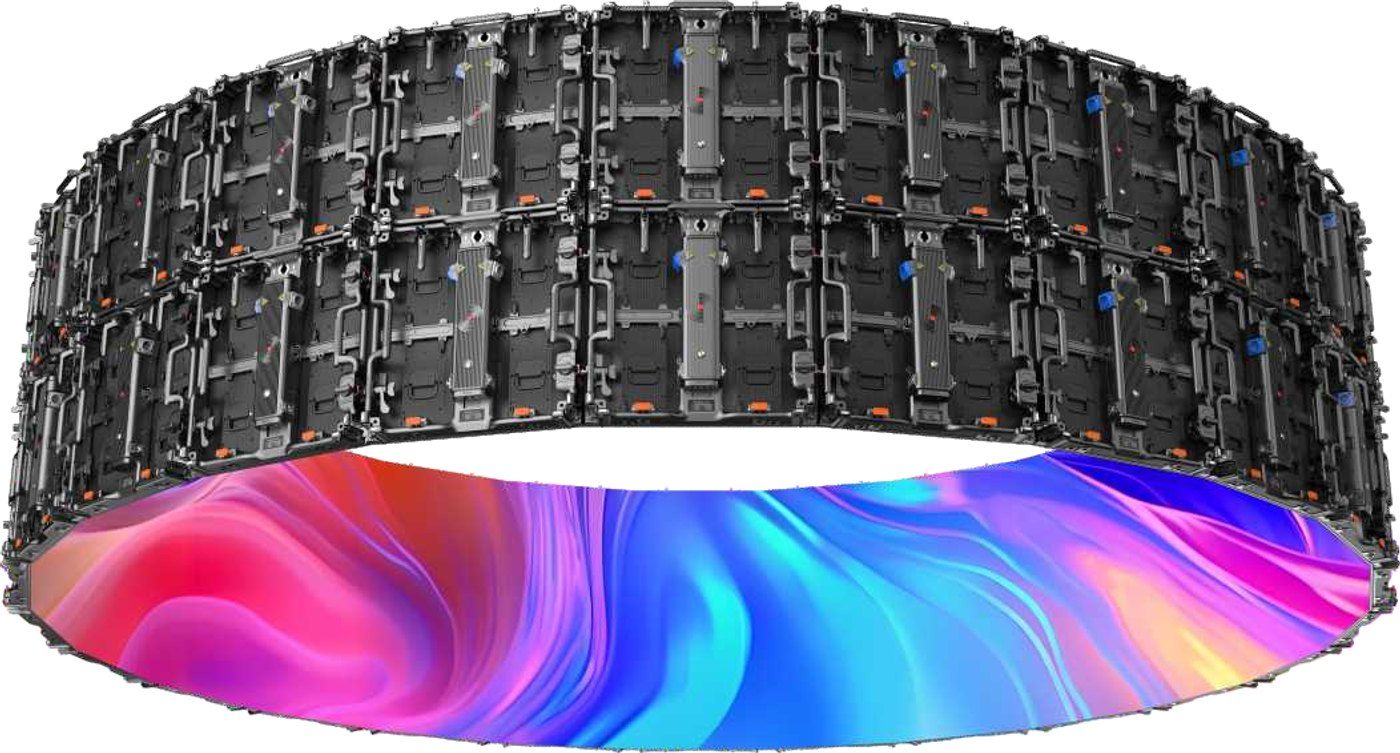
A shape and a surface technology are separate choices. A cube, a curve, a touring cabinet or a fine pitch dvLED wall can each be built in COB, MIP, SMD FC or SMD, so the room decides the shape and the picture decides the surface.
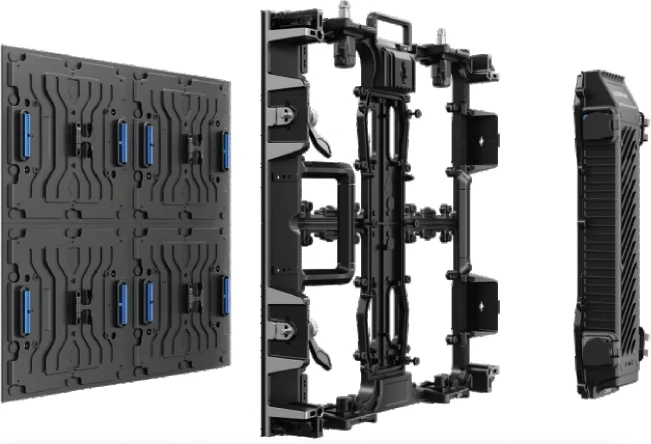
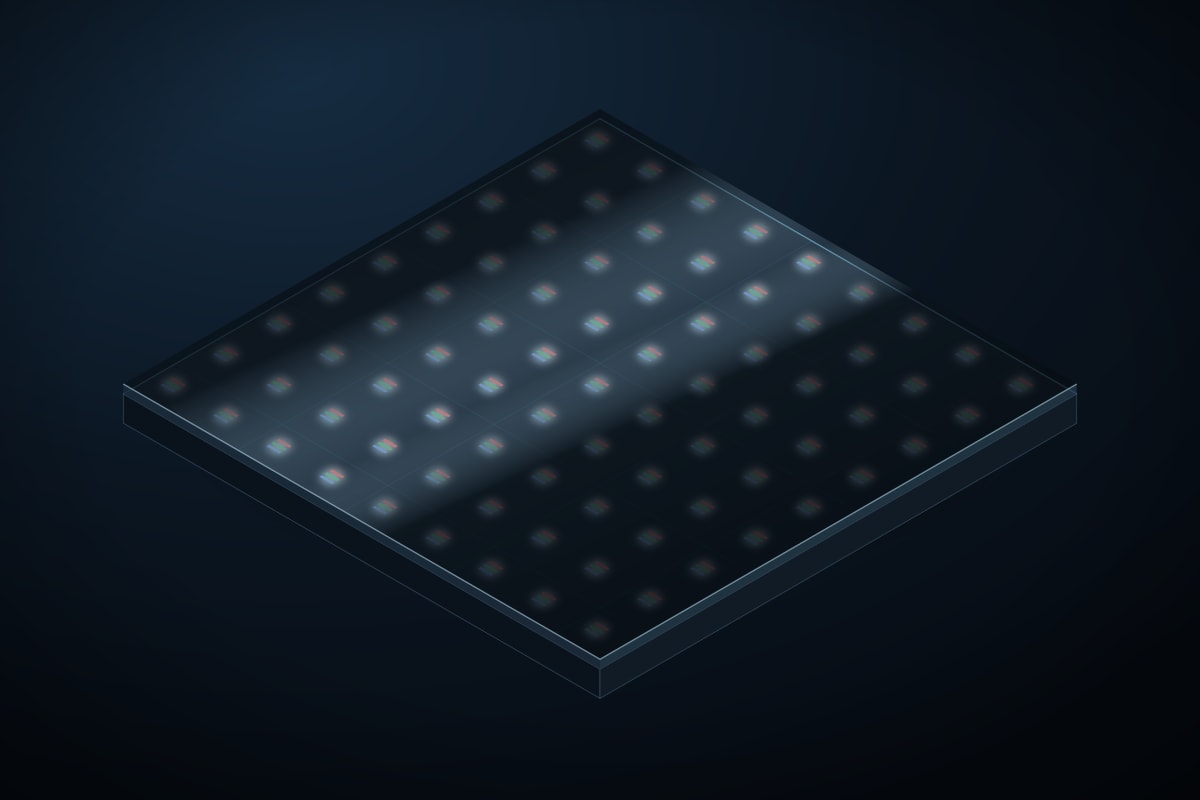
COBChip on board
The bare LED dies are mounted straight onto the board and sealed under a single smooth resin surface.
Nothing stands proud of the face, so there is nothing to knock off. The surface takes impact, sheds heat well and reaches the deepest black of any panel we build, which is why it holds a picture together in a dark studio.
The trade off: dies mounted this way cannot be measured and sorted the way finished packages can, so raw uniformity starts lower and calibration carries far more of the load. That is precisely where our own Color Space Engine earns its keep. And because a single sub pixel cannot be lifted out, service happens at module level rather than pixel level.
Best for: The finest pitches, any room where contrast decides the shot, and floors when a load bearing cover sits over the modules.
A sealed surface with nothing standing proud: COB takes knocks and sheds heat.
In a dark room, a studio or on a stage, its deep black holds the picture together where bright highlights sit next to shadow.
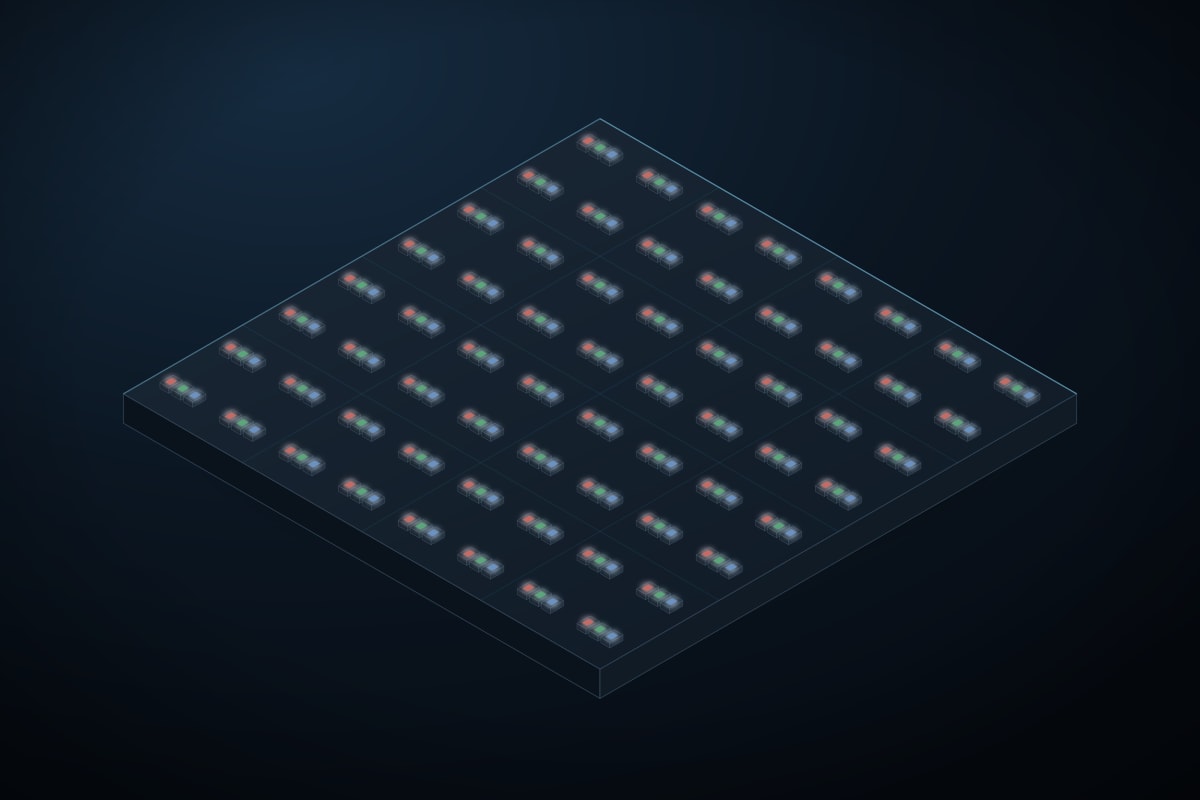
MIP & SMD FCMicro LED in package, and flip chip surface mount
Two routes to fine pitch that keep the advantage of a finished, measurable package.
Micro LED in package puts very small dies into their own tiny packages before they are placed on the board. Because every package can still be measured and sorted before mounting, uniformity and colour consistency start high and stay there from batch to batch. This is the main reason design studios choose MIP: the separate micro LED crystals can be binned and sorted far more finely before calibration, so homogeneity and colour accuracy are superior to COB by default. The small dies and the larger black area between them also mean minimal light reflection and high contrast.
Flip chip surface mount turns the die over and bonds it directly, with no wire crossing the top of the emitter. Less material above the light means more of it reaches the room for the same power, heat behaves better, and the package copes with pitches that would trouble a conventional build.
Best for: Colour critical rooms that also need serviceability, and long lived installations where batch to batch consistency matters.
A car at life size, in the same colour after years of daily reviews as on the day the dvLED wall was calibrated.
Design studios choose MIP because every micro LED crystal is binned and sorted before calibration, so homogeneity and colour accuracy are superior from the start.
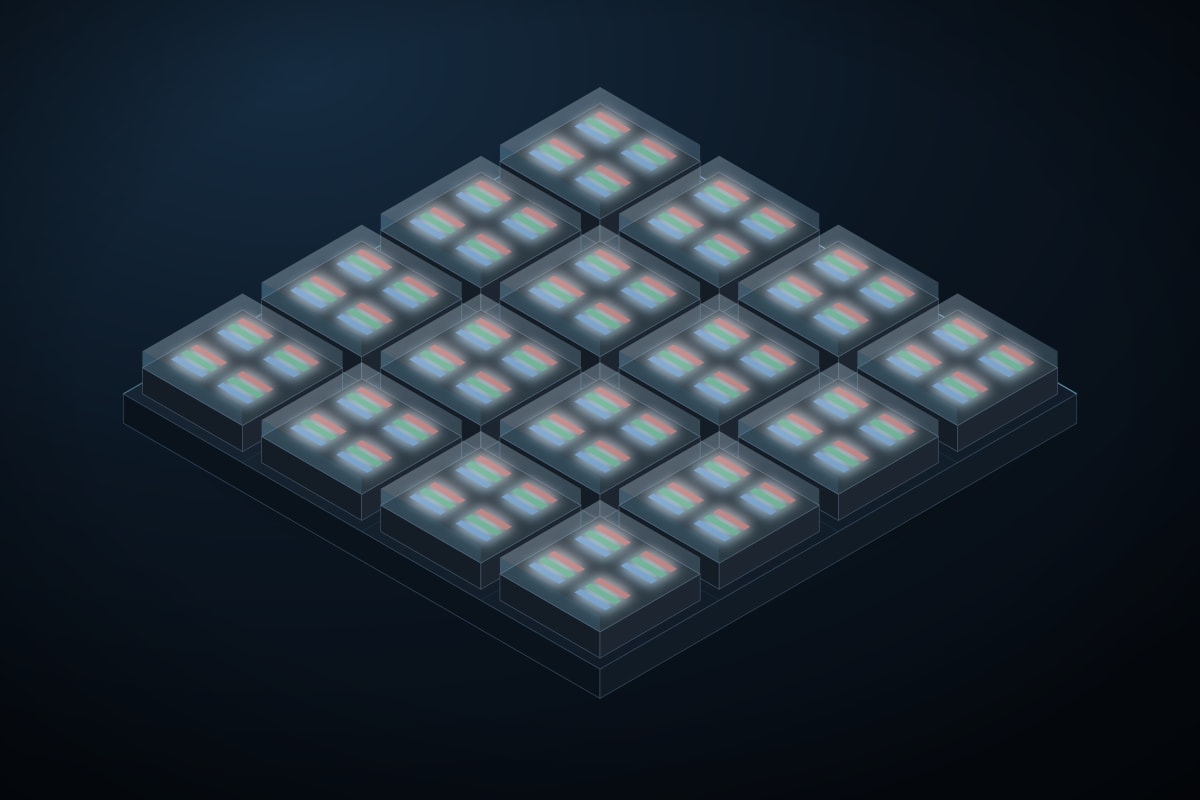
IMDIntegrated matrix device
Several pixels, usually four, gathered into one package.
This sits between surface mount and chip on board and takes something from each: fine pitch behaviour with straightforward manufacture and service, in a robust cabinet built to be rigged, struck and rigged again.
It is the family we reach for when a camera is in the room. High refresh and high frame rate keep the dvLED wall clean on sensor, with no banding rolling through the shot.
Best for: Virtual production and broadcast, rental and touring, and curved or cornered builds.
A camera sees what the eye forgives.
High refresh and a perfectly engineered sync behaviour keep the dvLED wall out of the shot.
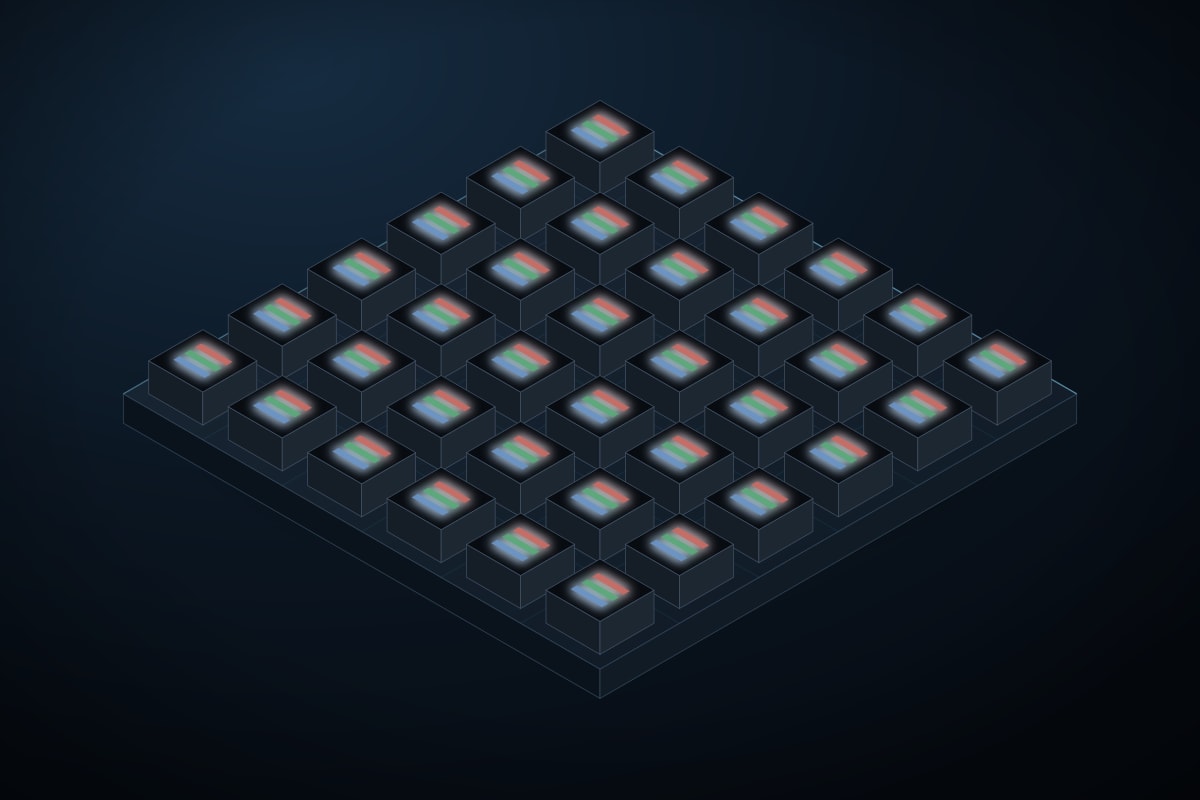
SMDSurface mount device
Individual red, green and blue LEDs placed onto the board. The most mature way to build a dvLED wall.
Proven, serviceable down to a single package, and the reason a large format screen can be affordable at all. This is also the chapter that goes outside and stays legible in direct sun, and the one that carries the flexible cabinets for curves and cylinders.
The trade off: at very fine pitches those small exposed packages become delicate, which is why the finest work belongs to chip on board and micro LED in package instead. Where a dvLED wall gets touched, dusty or rained on, a GOB protective coating can be specified on top.
Best for: Outdoor and daylight, large formats, curved and flexible builds, and projects where value per square metre leads.
Full sun, and the picture still holds.
More than 10000 nits and full protection from every side when the room is the outdoors.
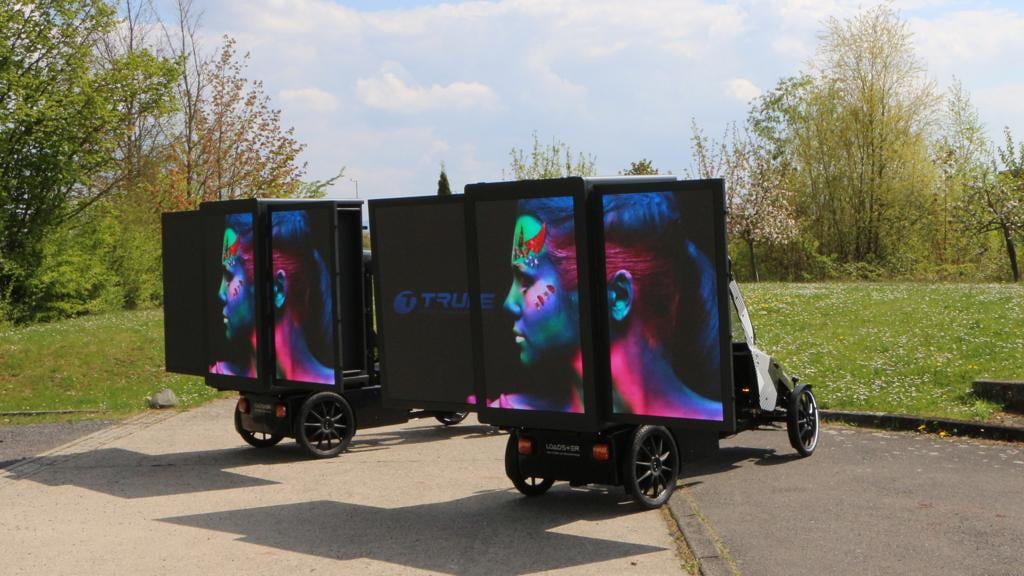
Some dvLED walls have wheels
Bright enough for daylight, sealed against weather, and light enough to be towed to where the audience already is. The same cabinets, on a trailer.
Which is the summary of this page: the surface, the shape and the cabinet are three separate decisions, and we make all three ourselves.
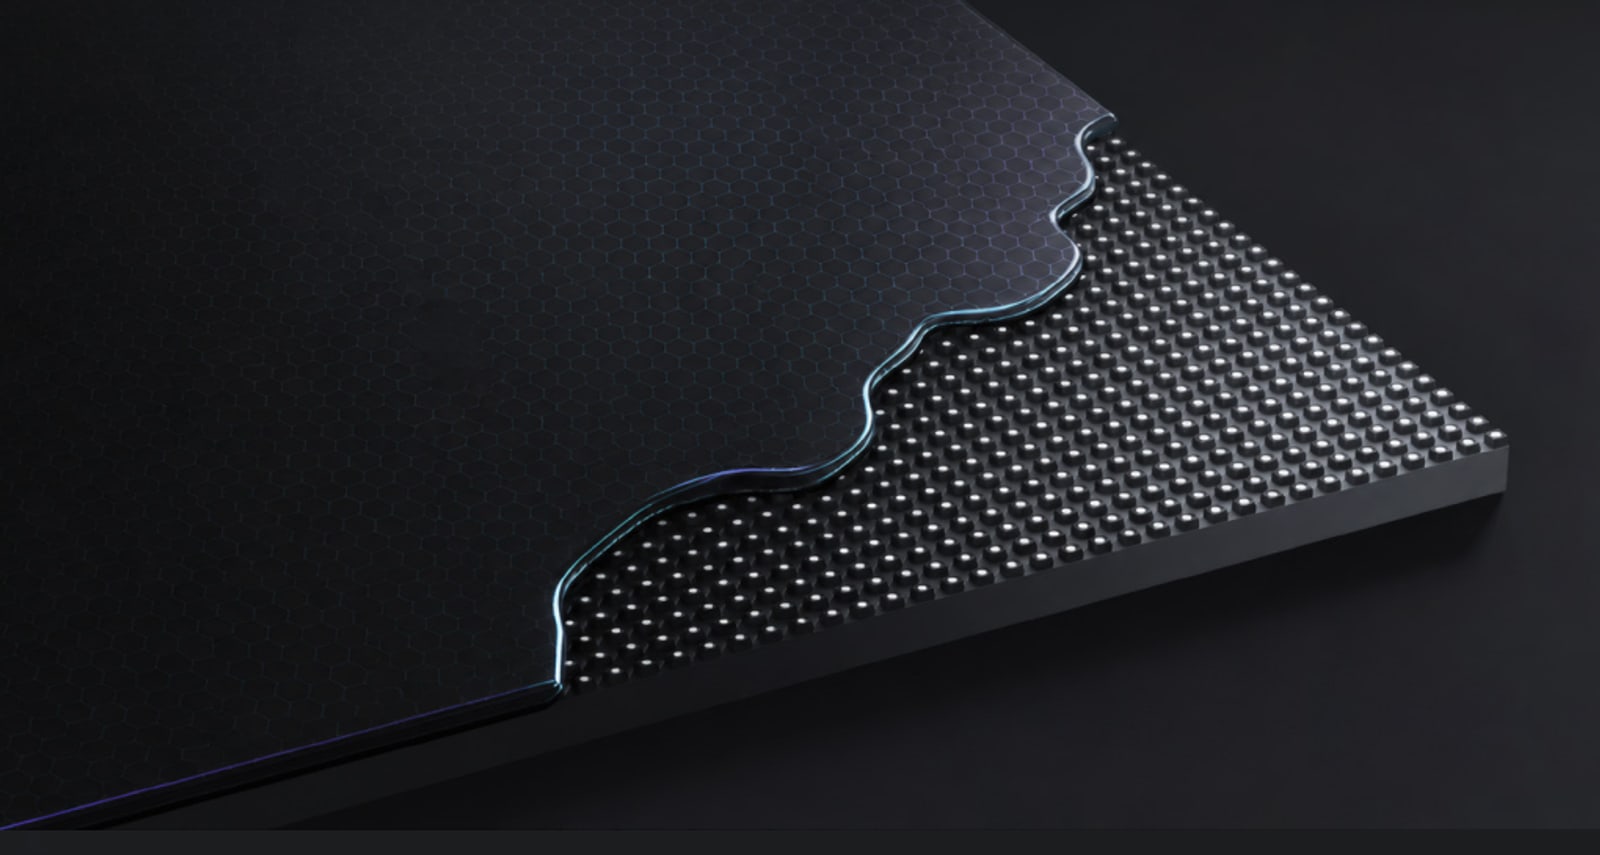
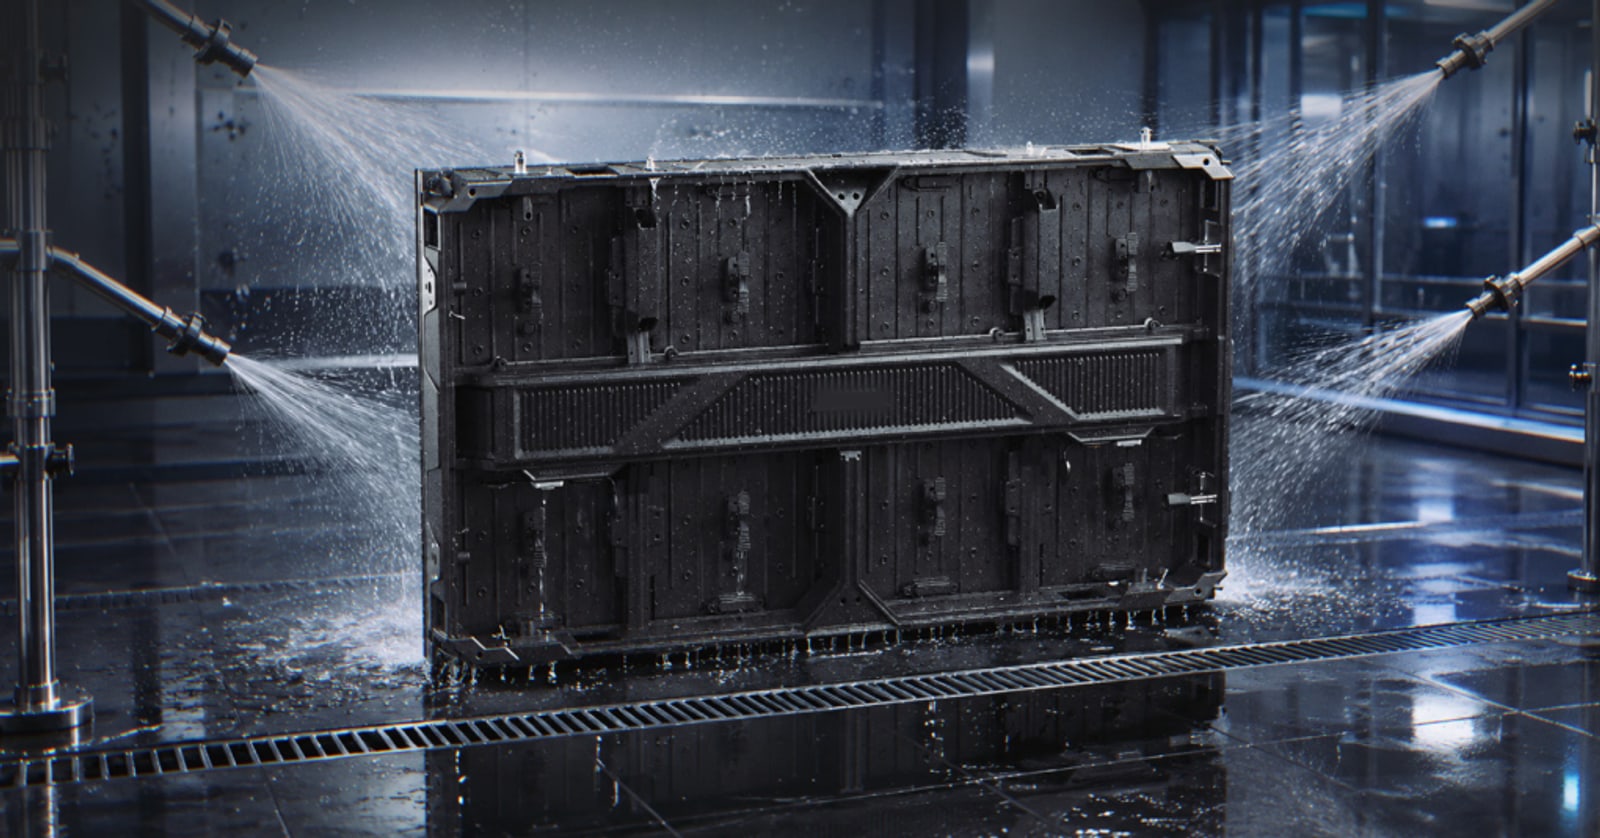
A surface is only as good as what it survives
Colour accuracy is the part you see. The rest of the engineering is the part you only notice when it fails, so it gets tested rather than claimed.
Everything around the dvLED wall
A dvLED wall arrives with more than cabinets. All of this is quoted per project rather than picked off a shelf, so tell us how the dvLED wall is used and we will tell you what it needs around it.
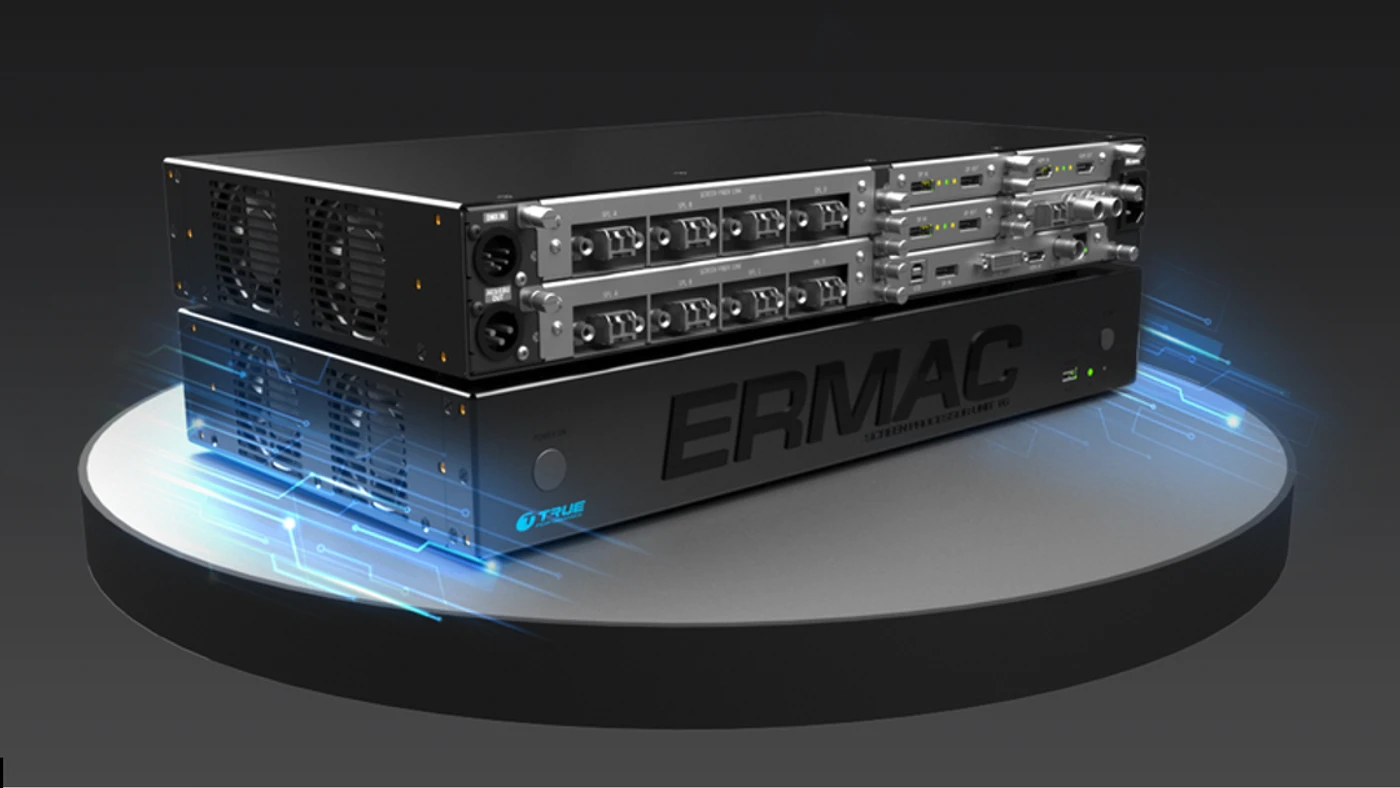
Control SystemERMAC processing, scaling and distribution
The half of the display that is not the panel, and the reason the colour holds.
Every TRUE dvLED wall is driven by ERMAC, our own control system, developed and produced in Europe. The SPU-32 does the processing, the LSC-108 handles scaling and distribution, receiving cards sit behind the panels, and input and output cards decide what arrives and how it travels.
Because the panel and the control system are engineered by one team, calibration is not a layer bolted on at the end. It is held in hardware, across brightness levels and across production batches.
Processing
- SPU-32
Receiving cards
- Receiving Card TRUE G-Series
- Receiving Card RC G40a
- Receiving Card RC G36Xi
Output cards
- Fibre Output Card (f4 | SFO110)
- Ethernet Output Card (e8 | SE111)
Input cards
- DP 1.4 Input Card
- HDMI 2.0b Input Card
- 12G SDI Input Card
Scaling and distribution
- LSC-108
- LSC Power Supply
- Cable Set LSC
Signal cabling
- Fibre Optic Cable 5 m
- Fibre Optic Cable 25 m
- Fibre Optic Cable 50 m
- Fibre Optic Cable 100 m
Playback
- Mini PC
Panel questions
What is the difference between XF+ and XR+ panels?
XF+ is the fixed installation series: fine pitch cabinets such as 600 × 337.5 mm, built flat to sit in a wall. XR+ is the rental and touring series in 500 × 500 and 500 × 1000 mm with handles and quick locks, built to be rigged, struck and rigged again.
Which pixel pitch do I need for my viewing distance?
Rule of thumb: the minimal viewing distance in meters equals the pixel pitch in millimeters. A 1.5 mm dvLED wall looks sharp from 1.5 m, a 2.5 mm dvLED wall from 2.5 m. Choose the largest pitch that still looks clean from where people stand, and go finer where they inspect the dvLED wall up close.
What does a GOB coating do?
A protective layer over the LEDs that takes impact, dust, moisture, UV and antistatic duty. It lets an SMD or MIP surface go into high traffic and outdoor situations that would otherwise be too delicate for it.
Which surface technology should I choose?
COB for the finest pitches, rooms where contrast decides, and floors when a load bearing cover sits on top. MIP and SMD FC for color critical rooms that also need serviceability and batch to batch consistency. IMD when a camera is in the room. SMD for outdoor, daylight, large formats and value per square meter.
Are all TRUE panels driven by the ERMAC control system?
Yes. Every TRUE dvLED wall is driven by ERMAC, our own control system developed and produced in Europe, with the Color Space Engine holding a Pantone validated reproduction. Where a project calls for it, we also deliver and support solutions built on NovaStar and Colorlight.
Tell us the room, we will tell you the panel
Pitch, brightness, viewing distance and whether a camera is in the room decide the surface technology between them. Size a dvLED wall yourself in the designer, or send us the room and we will come back with the panel and the control system that fit it.